Goodson Gazette
6 Ways To Improve the Performance of Your Hot Tank or Jet Washer
1. Keep tramp oil and sludge deposits out of your cleaning solutionTramp oil and sludge deposits make your solution less effective. Caustic is still trying to “clean” the leftover sludge and oil. Periodically, dip out or clean sediment from your machine. Your solution will last longer and be more effective on the parts you want cleaned.
Cleaning Tips
Most ferrous (iron or steel) parts may be cleaned in a hot soak tank, but never aluminum or zinc parts. Carburetors, fuel pumps and cam bearing should likewise never be put in a hot tank. Goodson’s D-CI25 Cast Iron Cleaning Detergent is a strong, alkaline that removes dirt, heavy oil and grease, carbon, light rust and paint.Maintaining The Other Machines in Your Shop
In several previous posts we’ve discussed various maintenance requirements for your big machines – surface grinders, crank grinders, cleaning machines, etc. Now we’re going to take a look at five other devices that play an important part in building the best possible engines for your customers – the air compressor, hydraulic press, brake lathe, bench grinder and seat grinding set.You Can’t Machine Until its Clean!
Here at Goodson, we talk a lot about cleaning. Why? Because "you can't machine until it's clean" and Goodson is all about machining. In this newly updated article about cleaning, Dave Monyhan (retired) explains how to clean your cleaning machines and make them work at peak efficiency.
3-angle Seat Cutting Tips
Carbide Pilots help keep tooling cutting true. When cutting 3-angle seats, counterboring for seat rings or using Bowl Hogs to enlarge valve bowls, the resistance of the workpiece against the tool tries to deflect the pilot. Goodson Carbide Pilots resist this deflection five times better to keep the tool cutting precisely in its path.
What’s that smell?
Let me paint you a picture of summer in your shop … the birds are chirping, the fish (and mosquitoes) are biting and everyone is enjoying the steamy days of summer. It’s late in the day, when you walk into your shop and suddenly you’re stopped dead in your tracks! There is a looming malodorous emanation in the air. “What is that smell? Where is it coming from? Do my customers smell it too?” I mean the smell is so bad, that even stink would say “Whew that stinks!”Cylinder Boring Tips
Lightweight block castings have become very prevalent in our market. Since the overall mass has been reduced, the controlled stresses have become an important factor in the block’s integrity. To ensure integrity, we must recreate that stress by using a Torque Plate when boring and honing.
Always begin by torquing your main caps in place to correct specifications. Next, install a torque plate and torque in place using final assembly torque specifications. Also, we recommend using correct length bolts. If they are too long or too short, they may abnormally stress the block. The future will even dictate correctly torquing all external motor mounts and related accessory brackets.
Allow .003″ minimum material in the cylinder bore. Remove broken and partially severed material by honing after the boring operation.
Choosing the power source for your portable hone
Portable hones may be driven by a heavy-duty electric drill, air drill or drill press. Optimum RPM is calculated by dividing 1200 by the bore diameter in inches (for example: 1200 / 6 inches = 200 RPM) or by dividing 30,000 by the bore diameter in millimeters (for example 30,000 / 150mm = 200 RPM). If the power source is a drill press or other rigid stroking device, make sure your portable hone is equipped with two universal joints to provide full floating action at the honing head.
Remember, if you have more questions, contact the Goodson Tech Department at 1-800-533-8010 (customers outside the US & Canada, please call 507-452-1830).
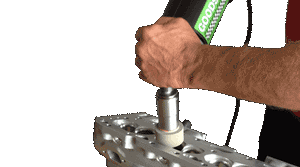
Take a seat – a valve seat that is
By way of introduction, let me say that this is going to be an “entry level” summary valve seat work.
I’ll assume that if you’re reading this, you know what a valve seat is and have at least a passing knowledge of why you grind or cut seats but just so we’re all on the same page, here’s the definition I’m working from:
The object of grinding or cutting is to obtain a valve seat of a specified, uniform width in the correct position on the valve face with minimal stock removal.